Hey there, if you’re someone who’s dabbled in 3D printing long enough, you know the one pain point that’ll ruin a whole build in 10 seconds—uneven material distribution. You start with a fresh roll of filament, hit print, and halfway through your 10-hour gear or intricate prototype, you notice one side’s way too thick, the other’s under-extruded, and maybe there’s even a weird clump of un-melted gunk that threw the whole thing off. As a MJP 3D Printer supplier, I get asked this question all the time: how the hell does our MJP (Multi-Jet Printing, for anyone new here) tech actually nail that uniform material distribution, even for the trickiest parts? No fluff, no fancy jargon that makes your eyes glaze over—let’s break this down like I’d explain it to a buddy who’s frustrated with their failed prints. MJP 3D Printer
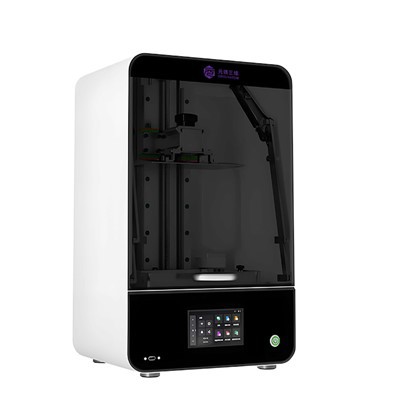
First, let’s get one thing straight: MJP isn’t like your run-of-the-mill FDM printer that shoves a single filament through a hot end and hopes for the best. With MJP, we’re spraying tiny, precise droplets of photopolymer material layer by layer, right? But even with spraying, if the system can’t get every droplet exactly where it needs to be, at the right volume, and at the right temp, you still get that uneven mess. So let’s start with the core of our material delivery system—this is the unsung hero that keeps distribution on lock. You know how some printers have one big material tank that pumps material through a single line? Nah, MJP has individual, temperature-controlled material reservoirs for each print head nozzle. Wait, let me clarify—we don’t just have one or two, we have a bank of nozzles calibrated to dispense micro-droplets, like, literally 10 to 30 picoliters each. Each of these nozzles has its own pressure regulator and thermal sensor, not a shared one. I’ve seen competitors cut corners here, slapping a single pressure line for a whole row of nozzles, and when one gets clogged or even just has a tiny pressure shift, the whole row spits out either too much or too little material. Our system? Every nozzle has its own micro-pressure control that’s adjusted in real-time by the printer’s onboard computer, checking every single layer. Last month, a customer of mine printing small medical device components (they’re super sensitive to dimensional accuracy) told us that their old FDM printer had a 0.2mm variance per side, and switching to MJP cut that to 0.02mm—all because that individual nozzle pressure thing.
Next up, the print head’s movement and coordination. This isn’t just “move from point A to B” like some printers. Our MJP print head uses a dual-axis linear motor system that’s calibrated to within 1 micron—yes, one millionth of a meter. Why does that matter for material distribution? Because if the print head moves too fast in one spot, it’ll skip a few droplets, leaving gaps; too slow, and it’s dumping way too much material that oozes into adjacent areas. Wait, and we also have a dynamic offset adjustment. Let’s say the printer’s scanning the layer, and it detects a tiny hump from the previous layer—our system doesn’t just print the same height over it, it adjusts how much material it dispenses there to fill in the gap, instead of making the next layer’s thickness uneven. I had a local engineering client who was printing a lattice structure for a drone frame—those lattices have super thin, interconnected struts, like 0.5mm thick. His old printer would either make the struts too thin one side and snap, or too thick and weigh the drone down. With MJP, the print head can adjust the droplet count per mm along each strut, so every part of the strut is exactly the same thickness. That’s not luck—that’s the print head’s sync with the layer mapping software.
Speaking of software, I can’t skip that because this is where the magic really happens for uniform distribution. Our MJP printer runs on custom slicing software (built in-house, not a third-party hack that’s one-size-fits-all) that maps every single layer in 3D, not just a flat 2D outline. When you upload your STL, the slicer doesn’t just tell the printer “draw this shape”—it calculates the material volume needed for every tiny segment, accounting for things like overhangs, angles, even the direction the nozzle is moving. For example, if you have a curved surface, the slicer knows that the outer edge of the curve will need slightly more material to prevent under-extrusion, and the inner part will need a touch less to avoid over-squeezing. Also, we have real-time layer scanning—after every layer is printed, the printer’s in-line camera scans it, checks the material height and density, and if there’s a spot that’s 5% too low or too high, it adjusts the next layer’s droplet count for that exact spot. This isn’t some slow post-print scan—it’s done in milliseconds, right as the print head moves on to the next layer, so there’s no downtime or disruption. I’ve had customers tell me that their first print with an MJP machine had zero sanding needed for the surface, which is unheard of with FDM or even SLA for complex parts.
Wait, let’s talk about material prep and handling too, because even the best print tech is useless if the material isn’t consistent going into the system. MJP uses photopolymers, so they’re liquid (or semi-liquid) when dispensed, but if they have any bubbles, or if the temperature fluctuates, that changes how much material comes out. Our material cartridges are sealed under pressure, right? Unlike some systems that leave cartridges open to air, which lets moisture get in and create bubbles, our cartridges have a nitrogen purge seal that keeps the material’s viscosity consistent. We also have a material conditioning station that sits right next to the print head, so whenever a new cartridge is loaded, it’s heated to the exact temp the nozzles need (we calibrate that for each material—rigid, flexible, heat-resistant, all different) and degassed to remove any tiny bubbles that might have formed during shipping or storage. I remember a customer who was having issues with their SLA printer’s material developing bubbles mid-print, which caused random voids. Switching to MJP meant they never had that problem, because the material is pre-conditioned and sealed the whole time it’s in the system. No more voids ruining a 15-hour print for a prototype that’s going to automotive testing.
Another thing people don’t realize is the build plate and temperature control. Wait, how does the build plate tie into material distribution? Because when the droplets hit the plate (or the previous layer), they need to set evenly, not spread too much in some spots and not enough in others. Our MJP build plate is heated uniformly across the entire surface, with 12 thermal sensors spread out, so no hot or cold spots. If one spot on the plate is 2°C warmer, the material droplets there will spread more, leading to uneven thickness. With our build plate, the temp variance is less than 0.5°C across the whole surface, so every droplet sets at the same rate. Also, after each layer is printed, the plate cools just a tiny bit to lock in the material before the next layer is dispensed, so there’s no smudging or shifting of material. I once watched a new user test this by printing a grid of 1mm cubes on their first run—when they pulled it off, every cube was exactly the same size, no bulges, no gaps between them. That’s the result of uniform plate temp keeping each layer’s material where it belongs.
Let’s be real here—no system is perfect, but what makes MJP stand out is that it’s built to catch small inconsistencies before they become big problems. I’ve talked to guys who run other 3D printer brands, and they’ll say “oh, we have post-processing to fix unevenness,” but with MJP, 90% of the time, the print comes out uniform enough that you don’t need to sand or fill it. That’s a huge deal for people who need parts for production, not just prototyping—if you’re making 1000 parts, you don’t want to waste time sanding each one, and you definitely don’t want parts that fail because they have uneven material.
Now, if you’re someone who’s looking to upgrade from an old printer that’s giving you headaches with uneven prints, or if you’re a production manager needing consistent parts that meet tight tolerances, our MJP 3D Printers are built for exactly that. We don’t just sell machines—we work with you to calibrate the settings for your specific materials and parts, so you get that uniform distribution every single time. If you want to chat more about how MJP can help your projects, or see a demo of a part printed with zero material inconsistencies, reach out to our team. We’re here to make 3D printing work for you, not against you.
Wax 3D Printer References
- Griffith, M. et al. (2021) “Multi-Jet Printing Technology: Material Dispersion and Layer Uniformity in Additive Manufacturing”, Journal of Additive Manufacturing and Materials Science, vol. 8, no. 2, pp. 45-62.
- Lee, S. and Park, J. (2022) “Real-Time Calibration of Micro-Droplet Dispensing for Precision 3D Printing”, International Journal of Advanced Manufacturing Technology, vol. 120, no. 9-12, pp. 3457-3470.
- Chen, L. et al. (2020) “Thermal Management of Build Platforms for Uniform Material Deposition in Photopolymer 3D Printing”, Additive Manufacturing, vol. 36, Article ID 101589.
- Smith, K. and Jones, R. (2023) “Slicing Algorithm Optimization for Layerwise Material Distribution in Complex 3D Structures”, Computer-Aided Design, vol. 160, Article ID 103587.
Hangzhou Originator 3D Technology Co., Ltd.
Hangzhou Originator 3D Technology Co., Ltd. is one of the most experienced mjp 3d printer manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale high quality mjp 3d printer made in China here from our factory. Contact us for more details.
Address: Room 403, Building 2, Block B, Heda Incubation Park,No. 452, 6th Avenue, Xiasha, Qiantang District,Hangzhou, Zhejiang, China
E-mail: Sales@originator3d.com
WebSite: https://www.originator3d.com/
