Working in complex parts manufacturing for over a decade, I’ve lost count of how many times customers have walked into our conference room, whiteboard in hand, asking: “Why does this custom component fail electromagnetic compatibility (EMC) testing when the prototype worked in simulation?” The answer, more often than not, comes down to a truth that’s easy to miss: complex parts don’t just “have” electromagnetic properties—their shape, material mix, and tiny, hard-to-see features shape those properties in ways that rigid, off-the-shelf parts never do. As someone who’s walked the production floor, tested parts in our in-house EMC lab, and sat through dozens of late-night troubleshooting calls with clients, I’m here to break down what makes these parts unique, and how we, as a complex parts supplier, turn that complexity into performance, not a headache. Complex Parts
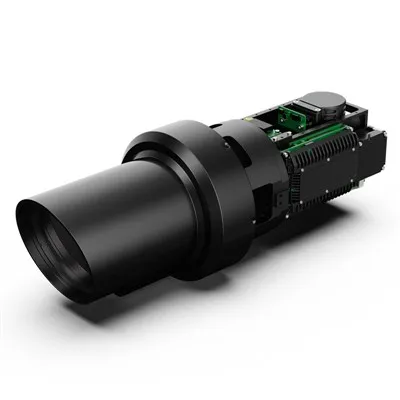
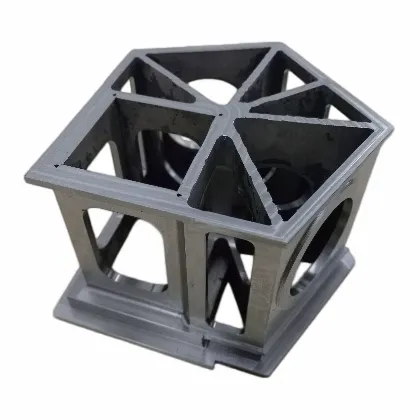
First, let’s define what “complex parts” actually mean in our line of work. These aren’t the injection-molded brackets or machined bolts you grab from a industrial catalog. We make aerospace engine mounts with integrated heat sink channels, medical device housings that blend hard carbon fiber with soft silicone gaskets for surgical tools, and automotive battery trays with embedded conductive busbars—parts with non-uniform geometries, multi-material layers, and small, intentional features (like sharp edges, tiny holes, or recessed slots) that solve functional problems but throw electromagnetic behavior way off. When it comes to electromagnetics, these features don’t just sit on the part—they interact with electric and magnetic fields in ways that would never show up in a simple rectangular block of aluminum.
Let’s start with electric field behavior, because that’s where most EMC failures start. Electric fields are all about charge separation: a part’s surface picks up or stores charge, and that charge leaks or radiates when it encounters a nearby electromagnetic source (like a smartphone or a satellite’s communication system). For simple parts, this is predictable: a solid metal bracket will have charge spread evenly across its surface, so leakage is easy to calculate. But take a complex part like the aerospace engine mount I mentioned earlier. It has internal coolant channels drilled into the center, so instead of a solid metal volume, it’s a lattice of aluminum with empty spaces. Those empty spaces disrupt charge distribution—sharp edges at the channel openings create local “hotspots” of charge density, right where electric fields are strongest. Last year, we had a defense client come to us because their new drone’s engine mount was causing interference with the on-board GPS. The simulation their in-house team ran used a solid aluminum model, which didn’t account for the channel edges. When we tested the actual prototype in our lab, we saw the charge hotspot at the channel entrance was radiating at 1.5 GHz, exactly the GPS frequency band. That’s the kind of gap between textbook electromagnetics and real-world complex parts that only comes from working hands-on with these components.
Then there’s magnetic field behavior, which is about current flow. Magnetic fields are generated when electricity moves through a material, and for complex parts, the path that current takes is never straight. Think about a medical implant housing we made last year for a pacemaker accessory: it’s made of a titanium outer shell with a thin gold-plated inner layer, and has tiny, precision-machined notches where the device’s wiring connects. When we ran EMC tests, we noticed the housing was generating stray magnetic fields that interfered with the implant’s lead signals. The problem? The gold-plated notches acted as unexpected current loops. In a simple, uniform part, current would flow along the shortest path, but the notches forced the current to take a U-turn around each edge, creating small current loops that radiated magnetic fields at low frequencies. Simple parts rarely have these intentional interruptions, so their magnetic field behavior is linear. Complex parts? Their magnetic response depends entirely on how those interruptions shape current paths—something simulation tools often miss if they’re not calibrated for multi-layer, non-uniform geometries.
Another key electromagnetic property of complex parts is their surface impedance. Surface impedance is basically a measure of how easily charge moves across a part’s surface, and it’s a huge factor in EMC, because high surface impedance means more charge buildup, which leads to more radiation. For off-the-shelf parts, surface impedance is consistent across the whole part—aluminum has a fixed impedance, steel has another. But complex parts? We often use multi-material construction, so surface impedance changes from one spot to the next. For example, when we make automotive battery trays, we combine conductive aluminum for structural support with insulating ceramic coatings on areas that contact the battery cells. That coating creates a tiny bump in surface impedance right where the tray meets the cell. If that bump is too high, charge builds up at the interface between the metal and the coating, creating a small electric field that can interfere with the battery’s management system. We learned this the hard way with a startup client two years ago: their initial tray prototypes failed EMC testing because we’d applied the ceramic coating too thick in a spot, creating that impedance bump. We adjusted the coating process to apply a uniform, micron-thick layer, and the test results dropped right into compliance. That’s the value of working with a supplier that’s not just machining parts, but also understanding how every process step impacts electromagnetic performance.
Now, let’s talk about the things that make complex parts uniquely tricky, but also uniquely capable when engineered right. One of the biggest challenges is resonant behavior. Simple parts have one resonant frequency—think of a metal plate that vibrates at a single tone when struck. Complex parts, though, have multiple resonant frequencies, because their irregular shape and multi-material layers create multiple pathways for electromagnetic waves to bounce around. For example, a wind turbine blade hub we made a few years back has embedded fiber-optic sensors and a steel core, so its resonant frequencies range from 100 MHz to 10 GHz. If a client’s control system operates at 2.4 GHz, that’s a problem—because the hub will resonate at that frequency, amplifying any stray electromagnetic signals and causing interference. The fix? We adjusted the length of the embedded steel core’s internal channels, which shifted the resonant frequency away from the client’s operating band. That’s not something a standard part supplier can do—you need to understand how every design tweak changes resonant behavior across a wide frequency range, not just the one your client initially specifies.
What many clients don’t realize is that electromagnetic properties of complex parts aren’t just about avoiding interference—they’re about designing for performance. For example, aerospace components often use intentionally complex geometries to shield sensitive electronics. A satellite’s sensor housing, for instance, has a corrugated outer shell that creates a maze of gaps and slots. Instead of letting electromagnetic radiation through, those gaps reflect and absorb the unwanted signals. This is called cavity resonance, and it’s a key property we leverage for shielding. But to make it work, we have to account for every gap’s width, depth, and material—even a 0.1 mm difference in a corrugation gap can change the shielding effectiveness by 20 dB, enough to make a satellite’s communication system go dark. We’ve had to rework a few housings over the years because a minor machining error threw off that gap dimension, so now we run a post-production EMC scan on every aerospace part we ship to catch those small, impactful issues.
So why does this matter for you, if you’re sourcing complex parts? Let’s be clear: if you’re using off-the-shelf parts, you can rely on standard EMC data from the manufacturer. But if your part is custom, has multi-material layers, or intricate features, you can’t. The simulation tools a lot of engineers use work great for simple geometries, but they often oversimplify complex parts, leading to costly reworks, delayed product launches, or compliance failures. That’s where our experience comes in. For over a decade, we’ve worked with clients across aerospace, medical, automotive, and defense, and we’ve built our process around testing and optimizing electromagnetic properties at every step—from design review to final production. We don’t just machine a part and send it out; we run EMC scans, simulate charge and current flow, and adjust features before the part ever hits your assembly line.
I’ll give you a recent example to drive this home. A medical device startup came to us six months ago with a custom handpiece for a surgical laser. The part had to blend a rigid medical-grade polycarbonate for the outer shell, a conductive copper layer for EMI shielding, and tiny ceramic insulators where the laser’s wiring connects. Their initial prototype, made by a different supplier, failed EMC testing because the copper layer had sharp edges at the ceramic insulators, creating charge hotspots that interfered with the device’s control panel. We took the original design, adjusted the edge profiles around the insulators to round them (reducing charge density by 40% in that area), and ran a full EMC simulation before machining the part. When we tested the final version, it passed first time. That’s the kind of attention to electromagnetic detail that only comes from working with complex parts day in and day out—we don’t see a part as just a hunk of metal or plastic; we see its electromagnetic signature, and we know how to tweak it to fit your needs.
If you’re reading this, chances are you’re working on a project where standard parts won’t cut it—where you need a component that’s lightweight, durable, and compliant with strict EMC standards. The last thing you want is to wait weeks for a prototype, only to find out it fails electromagnetic testing. The good news is that you don’t have to go it alone. We specialize in complex parts that are engineered with electromagnetic performance in mind, from initial design through final production. We don’t just deliver parts—we deliver solutions that work the first time, on time, and within your compliance requirements.
If you’re ready to stop dealing with EMC surprises and start working with a supplier that understands the unique electromagnetic properties of complex parts, we’re here to help. Reach out to our team to schedule a design review or prototype discussion, and let’s turn your complex part challenges into a competitive advantage.
SWIR Imaging References
- Balanis, C. A. (2012). Advanced Engineering Electromagnetics. John Wiley & Sons.
- Paul, C. R. (2006). Introduction to Electromagnetic Compatibility. John Wiley & Sons.
- Hansen, R. C. (2009). Radiating and Scattering by Complex Shapes. SciTech Publishing.
- ISO 11452-2:2019, Road vehicles – Component test methods for electrical disturbances from narrowband radiated electromagnetic energy – Part 2: Absorber-lined shielded rooms.
- ASTM E1344-18, Standard Test Method for Power Line Transfer Characteristics of Shielding Materials.
Xi’an Zhongke Lead Ir-Tech Co., Ltd.
We are one of the most experienced complex parts manufacturers in China, specialized in providing high quality OEM products with the industrial grade. We warmly welcome you to wholesale high performance complex parts at an affordable price from our factory.
Address: Building 8,Hard Technology Enterprise Community No.3000,Biyuan 2nd Rd,High-Tech Zone Xi’an,Shaanxi,China
E-mail: sales@lead-ir.com
WebSite: https://www.leadinfrared.com/
